Medical Device CDMO Blog & Insights
Expert articles, technical insights, and innovations in precision medical device manufacturing.
Latest Medical Device Manufacturing Articles
10 Cleanroom Assembly and Packaging Tips for Global Buyers
Table of Contents
- Cleanroom Grades: ISO Class 5 Limits ≥0.5 μm Particles to 3,520/m³
- Personnel and ESD Control: Follow ISO 14644-5 and ANSI/ESD S20.20
- Assembly Validation: Control Torque, Bioburden, and Critical Process Limits
- Packaging Qualification: Apply ISO 11607 and ASTM D4169 Distribution Tests
- Global Quality Records: Use ISO 13485, UDI, Lot Traceability, and AQL Sampling
- FAQS
- Conclusion
- Related Posts
Global buyers rarely evaluate a package by appearance alone. They examine particle control, material compatibility, traceability, sealing strength, and shipping resilience. Cleanroom Assembly and Packaging must therefore connect factory discipline with real-world handling.
ISO 14644-1:2015 defines airborne particle classification by concentration and particle size. EU GMP Annex 1 (2022) also expects a documented contamination control strategy. PDA Technical Report No. 13 remains a useful reference for environmental monitoring programs. These documents do not replace experience. They provide the framework for repeatable decisions.
Cleanroom microbiology expert Dr. Tim Sandle has emphasized that cleanrooms are controlled environments, not automatically sterile spaces. That distinction matters. A sealed tray can still fail through poor glove technique, weak heat seals, or careless labeling. Picture a double-bagged component leaving the room. Its outer surface may touch a cart, dock, or customs table before reaching the customer.
This guide presents ten practical tips for global buyers. It covers personnel flow, gowning, component preparation, packaging materials, seal verification, labeling, documentation, and transport testing. Each tip supports measurable risk reduction. Buyers should request particle data, bioburden results, seal-strength records, and lot-level traceability.
A perfect checklist does not exist. Supply chains change. Assumptions fail. That is why supplier audits, packaging trials, and corrective-action reviews remain necessary. The strongest programs combine standards with observed evidence, clear ownership, and honest communication when performance is imperfect.
Cleanroom Grades: ISO Class 5 Limits ≥0.5 μm Particles to 3,520/m³
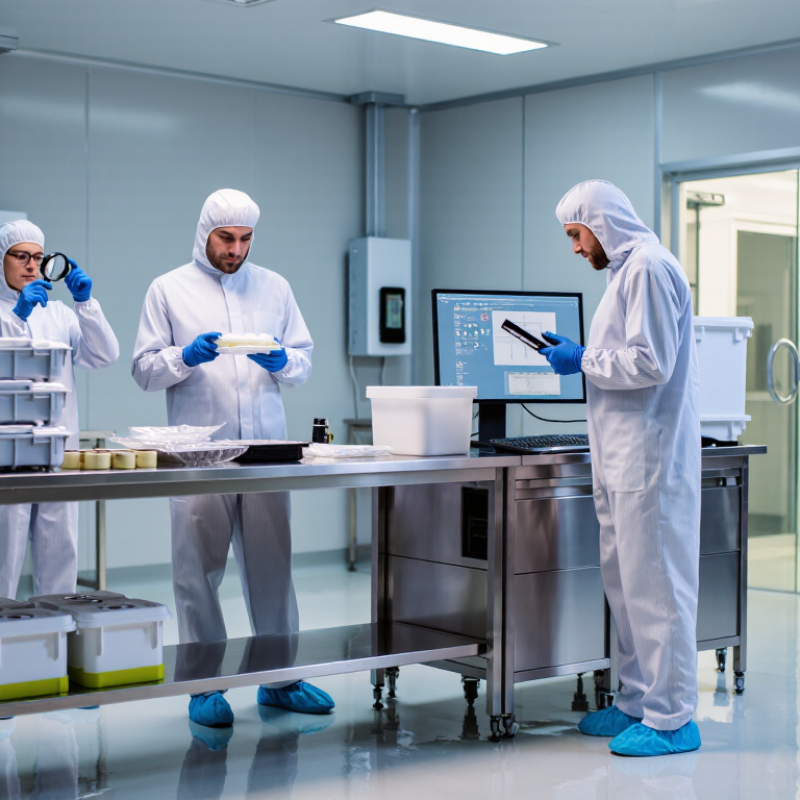
ISO 14644-1:2015 sets the ISO Class 5 limit at 3,520 particles per cubic metre for particles ≥0.5 μm. This is a concentration limit, not proof of sterility. The 2022 EU GMP Annex 1 reports the same Grade A limit for both at-rest and in-operation conditions. Global buyers should request the test method, sampling locations, and calibration records before approving assembly or packaging.
Packaging work can disturb settled particles. Operators should use low-shedding garments, cleaned tools, and sealed component transfer routes. Keep open product paths away from cardboard, paper, and unnecessary movement. Small details matter. A particle counter reading near the ceiling may miss turbulence around a tray or sealing station. ISO 14644-1 recommends risk-based monitoring, but practical layouts still require local studies.
Ask suppliers for particle recovery data after door openings, cleaning, and material transfers. Review environmental trends, not only one successful qualification report. Temperature and humidity records also matter when packaging materials change shape or attract dust. I have seen cleanroom plans look excellent on paper, yet fail during busy handoffs. That gap deserves scrutiny. Buyers should also confirm gowning training, cleaning validation, packaging integrity tests, and documented deviation handling. These records provide stronger evidence than a cleanroom certificate alone.
Personnel and ESD Control: Follow ISO 14644-5 and ANSI/ESD S20.20
Cleanroom assembly depends on disciplined people, not only filtered air. ISO 14644-5 supports controlled operations, gowning, material flow, cleaning, and documented procedures. Every operator should enter through a defined change area. Hair covers, gloves, masks, and garments must fit correctly. A loose cuff can expose a component to contamination.
ESD control requires more than wearing a wrist strap. ANSI/ESD S20.20 emphasizes a documented program, qualified equipment, grounding, training, and regular verification. Test personnel grounding before each shift when practical. Check footwear, wrist straps, work surfaces, and ionizers at planned intervals. Keep conductive packaging closed until parts reach the protected work area. A damaged tray needs immediate isolation.
Small habits matter.
During an audit, reviewers often examine training records, inspection logs, and corrective actions. They may also observe whether operators touch phones, cartons, or door handles before handling assemblies. Use visual prompts near entry points, but do not rely on signs alone. Supervisors should watch real work and refresh training after process changes.
Perfect compliance is difficult. Gloves tear, sensors drift, and busy operators miss a step. That weakness should be recorded, investigated, and corrected without hiding it. Global buyers can request calibration evidence, personnel qualification records, environmental monitoring data, and recent internal audit results. Clear records make technical claims more trustworthy.
10 Cleanroom Assembly and Packaging Tips for Global Buyers - Personnel and ESD Control: Follow ISO 14644-5 and ANSI/ESD S20.20
| No. | Control Area | Relevant Guidance | Recommended Practice | Buyer-Focused Verification Point | Typical Evidence |
|---|---|---|---|---|---|
| 1 | Personnel Entry and Gowning |
ISO 14644-5 Personnel and gowning procedures |
Use a documented entry sequence with hand hygiene, controlled changing areas, suitable cleanroom garments, hair and beard coverage where applicable, and cleanroom-compatible footwear. | The procedure is posted, trained personnel follow the same sequence, and gowning supplies are available before entry. | Approved gowning procedure, training records, entry checklist, periodic observations |
| 2 | Personnel Training and Behavior |
ISO 14644-5 Personnel practices and contamination control |
Train operators to minimize rapid movement, unnecessary talking, exposed skin, contact with critical surfaces, and unauthorized materials inside the controlled area. | Training covers contamination risks, workflow discipline, incident reporting, and refresher intervals defined by the quality system. | Training matrix, competency assessment, refresher-training log, deviation reports |
| 3 | Cleanroom Classification and Monitoring |
ISO 14644-1 Air cleanliness classification ISO 14644-5 |
Define the required cleanroom classification for each assembly and packaging activity. Monitor conditions using a risk-based plan for airborne particles, temperature, humidity, and pressure differentials where relevant. | Limits are documented by process area, monitoring instruments are calibrated, and excursions trigger documented evaluation before product release. | Room classification report, environmental monitoring records, calibration certificates, excursion investigations |
| 4 | Material and Component Transfer |
ISO 14644-5 Material flow and transfer controls |
Separate personnel and material flows where practical. Remove outer shipping cartons before entry, wipe compatible surfaces with approved materials, and use defined staging or pass-through procedures. | Material routes prevent avoidable cross-contamination, packaging layers are clearly identified, and transfer responsibilities are assigned. | Material-flow map, transfer SOP, cleaning log, incoming inspection record |
| 5 | ESD Protected Area |
ANSI/ESD S20.20 ESD control program requirements |
Establish an ESD Protected Area with defined boundaries, approved equipment, grounding points, access rules, and signage. Limit nonessential insulative materials near exposed electronic assemblies. | The ESD area is identifiable, controlled items are listed, grounding arrangements are documented, and access is limited to trained personnel. | ESD control plan, area layout, equipment list, grounding diagram, signage inspection |
| 6 | Personnel Grounding |
ANSI/ESD S20.20 Personnel grounding and compliance verification |
Use a suitable personnel grounding method, such as a wrist strap system or footwear-and-flooring system, selected according to the work activity and site risk assessment. | Grounding checks are completed at the required frequency, failed checks prevent access to exposed product, and corrective actions are recorded. | Daily test logs, tester calibration records, failed-test reports, corrective-action records |
| 7 | ESD-Safe Workstation Setup |
ANSI/ESD S20.20 Technical requirements for ESD control items |
Ground dissipative work surfaces and exposed conductive equipment according to the approved grounding scheme. Use suitable ionization where insulators cannot otherwise be controlled. | Workstations meet defined resistance-to-ground or resistance-to-groundable-point criteria, and ionizers are verified where used. | Resistance test results, ionizer verification records, workstation inspection checklist |
| 8 | Handling and Assembly Discipline |
ISO 14644-5 Contamination control practices ANSI/ESD S20.20 |
Handle parts by approved noncritical surfaces, use clean and ESD-safe tools, keep protective packaging closed until needed, and avoid stacking or dragging components across work surfaces. | Tools and containers are identified as cleanroom- and ESD-compatible, and operators follow defined handling points and exposure-time controls. | Tool qualification list, operator checklist, process audit, nonconformance records |
| 9 | Packaging and Labeling |
ANSI/ESD S20.20 ESD protective packaging requirements Customer-specific cleanliness controls |
Package exposed ESD-sensitive items in suitable shielding or dissipative packaging. Use clean inner packaging, secure closures, and labels that identify handling, orientation, lot, and traceability information. | Packaging protects the product during expected transport and storage conditions, labels are legible, and packaging materials are approved before use. | Packaging specification, material approval, label verification, packing inspection report |
| 10 | Audits, Maintenance, and Continuous Improvement |
ISO 14644-5 Operational control and maintenance ANSI/ESD S20.20 Compliance verification plan |
Conduct scheduled audits of personnel practices, environmental conditions, grounding systems, workstations, tools, packaging, and records. Review trends and investigate recurring failures. | Audit frequency, responsible owners, escalation rules, and closure deadlines are defined. Product-impact assessments are completed for significant deviations. | Internal audit reports, preventive-maintenance logs, trend charts, corrective-action plans, management review inputs |
Assembly Validation: Control Torque, Bioburden, and Critical Process Limits
Assembly validation turns a cleanroom procedure into measurable evidence. Torque deserves special attention because small variation can change seal compression, connector performance, or particulate generation. Use calibrated digital torque tools, recorded operator identification, and controlled tightening sequences. A practical internal benchmark is Cpk ≥1.33, although this is not a universal regulatory requirement. Recheck it after tool maintenance, product changes, and training updates.
Bioburden control needs more than a cleanroom classification. ISO 11737-1 describes methods for recovering and counting microorganisms, but it does not provide one universal acceptance limit. Set limits from product risk, historical data, and sterilization capability. For context, ISO 14644-1 allows up to 3,520 particles per cubic meter at 0.5 micrometers in an ISO 5 environment. That number does not prove microbial control. It only describes airborne particles. Sample gloves, components, and contact surfaces separately.
Critical process limits should be visible at the workstation. Define torque range, dwell time, alignment force, temperature, humidity, and exposure time. Use designed experiments when interactions are unclear. The FDA Process Validation Guidance recommends linking process parameters with product quality attributes, not merely checking final samples. Packaging teams should also challenge seal strength and integrity using recognized methods, such as ASTM F88 and ASTM F1929. Keep raw data, deviations, and retraining records available for global buyer audits. The uncomfortable part is simple: a validated process can still drift. Our own weak point is often not the protocol, but inconsistent review after minor changes.
Packaging Qualification: Apply ISO 11607 and ASTM D4169 Distribution Tests
Packaging qualification protects sterile products from real distribution hazards, not just laboratory appearance. ISO 11607-1:2019 requires packaging systems to maintain sterility until opening. ISO 11607-2:2019 also requires validated forming, sealing, and assembly processes. Treat each seal as evidence.
ASTM D4169-22 provides distribution cycles for shock, vibration, compression, and atmospheric conditioning. Select the cycle using actual shipping data, including pallet height, transport mode, and handling risks. A 2023 report from Smithers projects the global medical packaging market will surpass 30 billion dollars by 2028, increasing pressure for measurable validation. Do not rely on a single drop test. Test loaded cartons after conditioning, then inspect seals, pouches, labels, and product movement.
Use worst-case configurations. That means the smallest carton, heaviest load, longest transit, and weakest acceptable seal. Record temperature and humidity before testing. Packaging engineers often find failures at corners, not panel centers. ASTM D4169 results should connect directly with ISO 11607 seal-strength, integrity, and aging evidence. A 2022 healthcare packaging survey by PMMI reported continuing concern about material availability and supply resilience, so alternate materials need separate qualification.
Real shipments can be messier. Pallets tilt. Cartons get wet. Qualification may still miss unusual handling. Review complaints, transit photos, and damage data every quarter. Perfect validation is impossible. Defensible learning is not.
Packaging Qualification Standards for Global Buyers
This timeline highlights commonly referenced standards for sterile barrier packaging, packaging process validation, accelerated aging, and distribution testing. Always confirm the applicable edition and test requirements for the intended market and distribution cycle.
Global Quality Records: Use ISO 13485, UDI, Lot Traceability, and AQL Sampling
For global buyers, cleanroom workmanship is only half the quality story. ISO 13485 controls documented processes, training, suppliers, nonconformities, and corrective actions. The ISO Survey 2022 counted more than 30,000 valid ISO 13485 certificates worldwide. That scale shows the standard’s importance, not automatic product quality.
Each assembly record should show operator identity, equipment status, material approval, and revision control. UDI data must connect the device identifier with its lot, production date, and packaging level. One missing digit can weaken recall accuracy.
Small errors matter.
AQL sampling makes inspection decisions more consistent. Use ANSI/ASQ Z1.4, then record lot size, inspection level, AQL, sample quantity, and acceptance number. Keep failed samples and inspection images when possible.
FDA’s 2023 device recall records list more than 1,000 recall events, reminding buyers that packaging and labeling deserve equal attention. Seal strength, print contrast, pouch damage, and foreign particles need defined checks.
Retain environmental monitoring logs beside lot records, not in separate folders. In practice, polished spreadsheets can hide weak evidence. Reviewers should test one lot from receiving through final shipment.
Some teams still treat UDI as a label task. That is risky.
A controlled data review before release can expose mismatched dates, duplicated identifiers, or incomplete supplier records.
FAQS
Filtered air is not enough. Operators control contamination through gowning, movement, handling, and documented routines.
Use the defined change area. Check hair covers, gloves, masks, and garments. A loose cuff can expose components.
No. The program also needs grounding, qualified equipment, training, work-surface checks, and regular verification.
Test personnel grounding before each shift when practical. Check footwear, wrist straps, surfaces, and ionizers at planned intervals.
Isolate it immediately. Keep protective packaging closed until parts reach the protected work area.
Test loaded cartons for shock, vibration, compression, and conditioning. Inspect seals, labels, pouches, and product movement afterward.
Use realistic worst cases: the smallest carton, heaviest load, longest transit, and weakest acceptable seal.
Keep operator identity, equipment status, material approval, revisions, lot details, inspection results, and environmental records together.
Record lot size, inspection level, sample quantity, and acceptance limits. Keep failed samples and inspection images when possible.
Gloves tear. Sensors drift. Busy operators miss steps. Record these failures, investigate them, and correct them openly.
Conclusion
Cleanroom Assembly and Packaging requires a disciplined approach to contamination control, process consistency, and product protection throughout the supply chain. For critical assemblies, ISO Class 5 environments limit particles at or above 0.5 μm to 3,520 per cubic meter. Personnel must follow appropriate gowning, hygiene, and behavior controls, while electrostatic discharge protection should align with ISO 14644-5 and ANSI/ESD S20.20. Assembly validation should define and monitor key parameters such as torque, bioburden, and other critical process limits to ensure repeatable results.
Packaging must be qualified to protect products during handling, transport, and storage. Applying ISO 11607 principles together with ASTM D4169 distribution testing helps verify package integrity and shipping durability. For international buyers, complete quality records are equally important, including ISO 13485-based documentation, UDI management, lot traceability, inspection results, and suitable AQL sampling plans. Together, these practices support reliable manufacturing, transparent quality control, and consistent delivery across global markets.
Blog Tags: